Precision centerless grinding & close-tolerance post-plate grinding — Des Moines, WA, serving Everett to Tacoma
We Make It Round
LL Centerless Grinding We Make It Round
LL Centerless Grinding does one thing: precision centerless grinding — bare steel and close-tolerance post-plate work — prototype runs to production lots, held to aerospace tolerances. Setup done properly, size held across the lot, and no part shipped that wasn’t checked.
We do one thing and do it well: centerless grinding — bare steel or plated. Send a print — or the part itself — and you’ll have a quote back the same week.
Precision Centerless Grinding
Thru-feed and in-feed centerless grinding on close-tolerance work. Setup is the whole job — blade angle, wheel dress, work height — and getting it right is what makes parts come off round, straight, and repeatable across the whole lot, not just the first ten.
Diameter range.250" – 7.1"
Tolerance±.0001" standard · ±.00005" achievable on suitable work
Surface finishTo 4Ra
Materials52100, 4340, 15-5 PH, Inconel, ToughMet, Al-Ni bronze — and more
Turnaround7–10 days, expedite available
Close-Tolerance Post-Plate Grinding
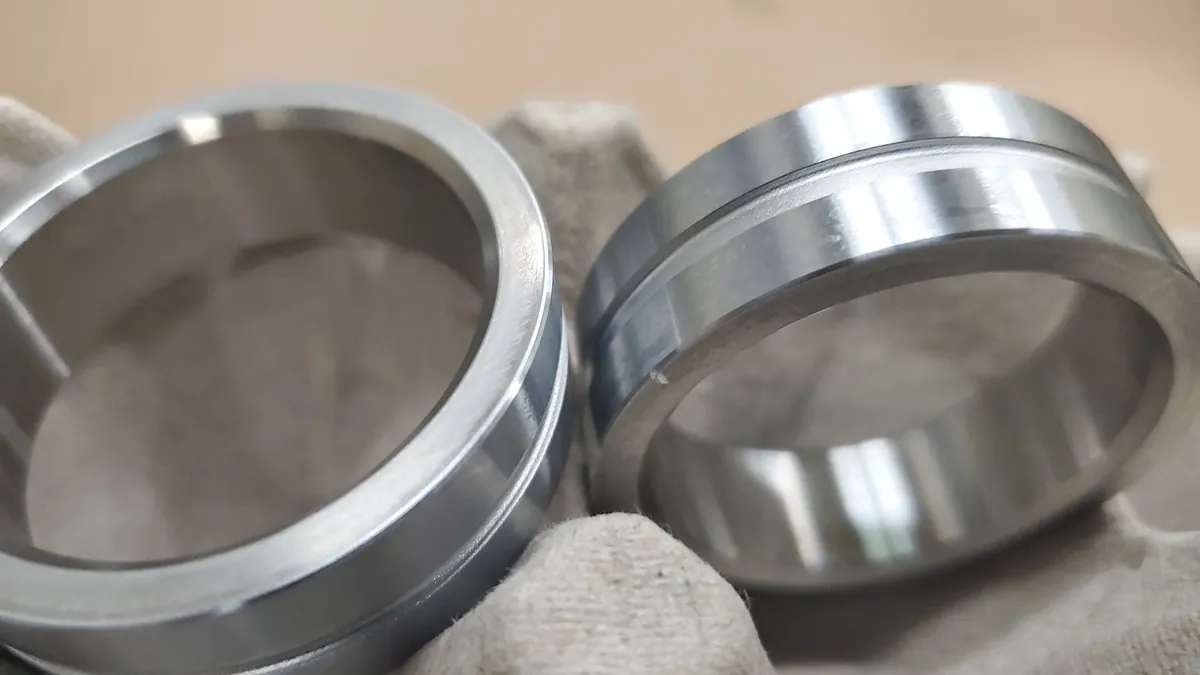
Hard chrome and electroless nickel ground to final size after plate. Plating never builds uniform, and chrome at Rc 65–70 punishes a wheel that isn't dressed for it — grind it wrong and you get burn, not size. Experience grinding to BAC 5032 (grinding of chromium plate) and BAC 5440 (machining and grinding of steel), including landing gear parts at 275 KSI and above.
CoatingsHard chrome, electroless nickel
Pre-plate grindingTo undersize, stock left for deposit
Tolerance±.0001" standard · ±.00005" achievable on suitable work
Surface finishTo 4Ra
Spec experienceBAC 5032, BAC 5440
Turnaround7–10 days, expedite available
Platers: we grind your customers’ chrome and EN to final size — parts back across the corridor.
Thread majors: major-diameter grinding on threaded parts.
Hands-on experience grinding to BAC 5032 and BAC 5440, including 275 KSI landing gear — not currently a D1-4426 approved source. Work runs to your print under your quality flow-down. Need an approved source? D1-4426 listing is by customer sponsorship — we’re open to that conversation.
Parts we grind
If it’s between Ø.250″ and Ø7.1″, we make it round — and hold size whether you send one part or ten thousand.
Blue marks the surfaces we can grind — diameters, fillet radii, and thread or spline majors. ↻ Drag any part to turn it over in your hands — let go and it falls back in step.
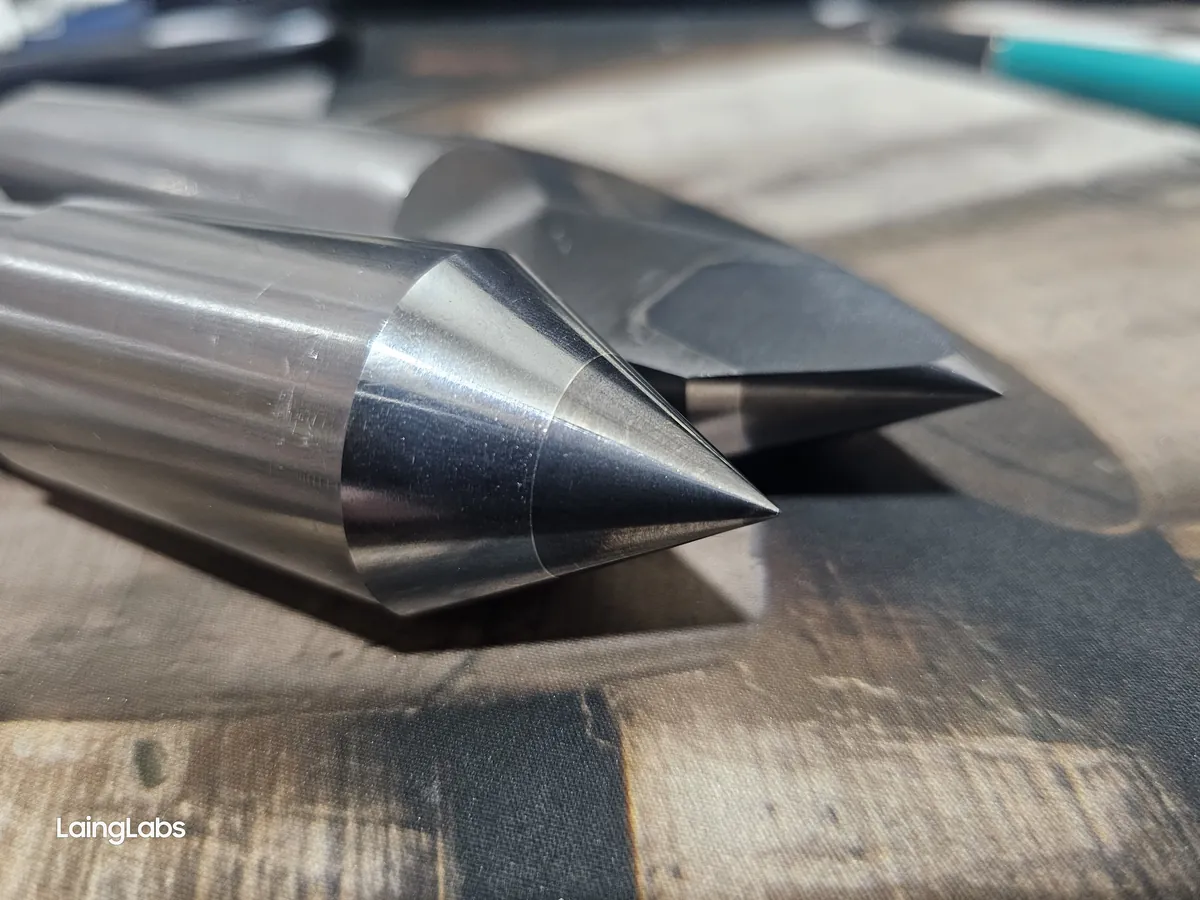
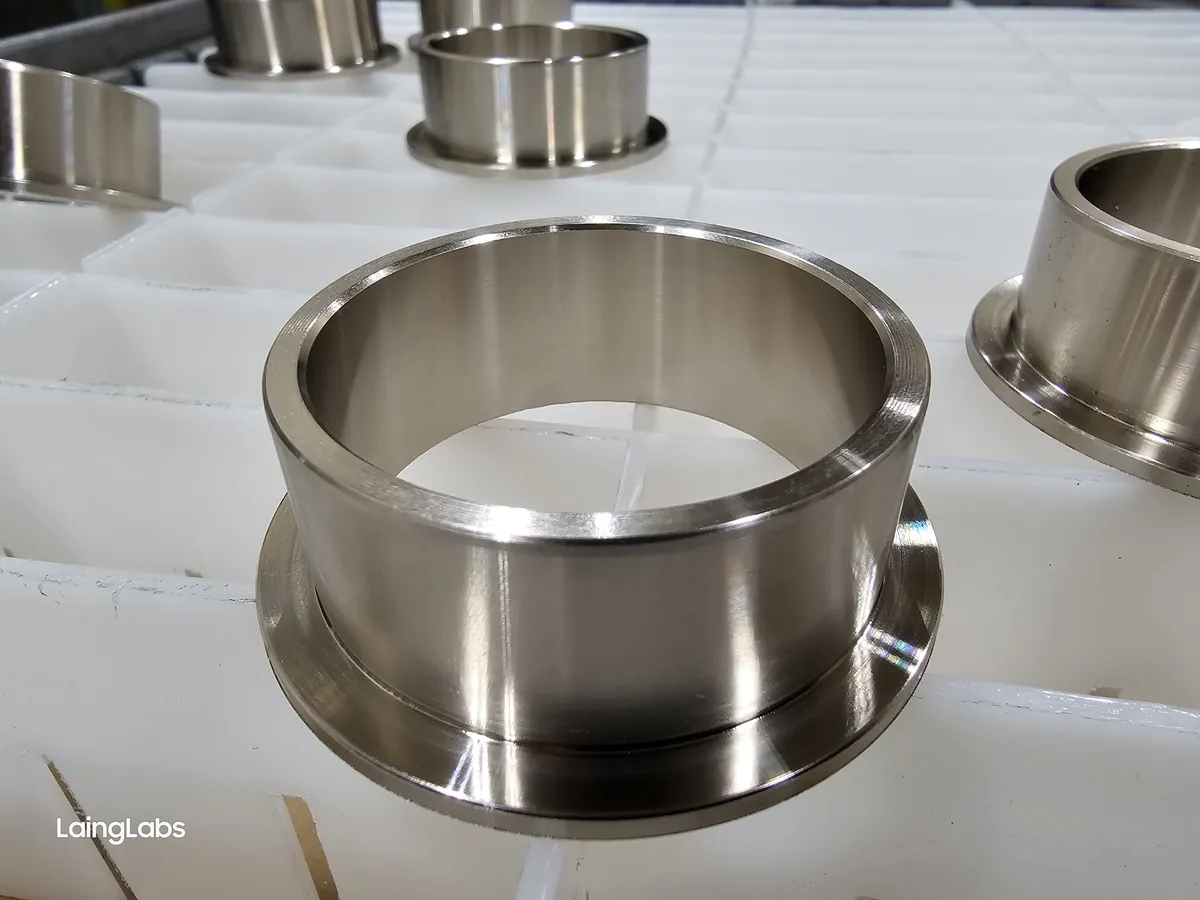
Dowel pinsThru-feed — plain diameters, ground end to endShafts & barThru-feed — long work, straight and roundShouldered pins & stepped shaftsIn-feed — both diameters and the fillet radius groundPlated pins & journalsPost-plate — chrome / EN ground to final sizeActuator & piston rodsPost-plate — hard chrome ground without burnValve stemsIn-feed — thin stems supported the whole cut, no deflectionFlanged bushings & sleevesIn-feed — thin sidewalls, both diameters and the fillet radius groundThin-wall tubingThru-feed — light wheel pressure, round without crush or chatterBearing rollers & small pinsThru-feed — 52100 and similar, lot after lotThread majorsThru-feed or in-feed — major diameter ground on threaded partsShoulder boltsIn-feed — shoulder Ø and thread major Ø ground concentricOD spline majorsIn-feed — spline major Ø ground on shaft ends, quoted case by case
Process experience: BAC 5032 · BAC 5440 |
275 KSI landing-gear work |
±.0001″ standard · ±.00005″ achievable |
4 Ra finishes
Grinding chrome is where the trade gets honest. A plated part is already expensive by the time it reaches the wheel, and burning one doesn't just scrap the part — on high-strength steel it puts untempered martensite where nobody can see it. That's the reason specs like BAC 5032 exist, and the reason careful setup beats fast setup every time.
That work has included landing gear parts at 275 KSI and above — the tier where a bad grind doesn't make scrap — it makes a part that fails in service.
LL Centerless Grinding is a grind shop in Des Moines, Washington — minutes from the Kent and Auburn plating and machining corridor. The trade was learned holding aerospace tolerance on production work, and the shop is built around the same standard: setup done properly, size held across the lot, and no part shipped that wasn't checked.
Equipment
Small shop, kept honest. Every part is set up and checked by the same pair of hands.
Cincinnati 220-8 centerless grinderThru-feed & in-feed, Ø.250″–7.1″ — the machine the shop is built around
Bridgeport milling machineFixturing & secondary ops — so a ground part ships finished